29
SeptemberApplications of Ultra High Purity Chemical Delivery Systems
An Ultra high purity chemical delivery system is a specialized facilities developed to transport extremely purified chemicals from storage containers to handling devices without endangering their quality. These systems are important in markets where contamination, bits, moisture, or undesirable chain reaction can adversely impact making procedures.
Unlike conventional chemical distribution tools, high-purity systems need thoroughly selected products, accurate engineering, controlled atmospheres, and trustworthy surveillance. Every phase of chemical activity must be thought about to protect the called for purity level from the factor of storage to the final application.

Significance of Maintaining Chemical Purity
Chemical purity is particularly essential in innovative production since small impurities can affect item performance and procedure uniformity. Semiconductor fabrication, pharmaceutical production, biotechnology, and specialized materials manufacturing usually entail processes with incredibly strict quality demands.
An Ultra high purity chemical delivery system helps reduce potential contamination triggered by devices surfaces, ecological direct exposure, particles, or inappropriate materials. Preserving constant chemical top quality can sustain repeatable manufacturing and lower the possibility of procedure interruptions. Appropriately developed shipment framework for that reason becomes a vital part of total manufacturing quality monitoring.
Key Elements and System Layout
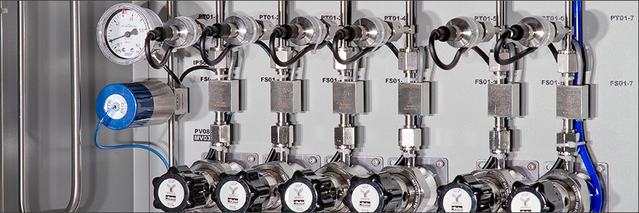
A high-purity chemical circulation network can have storage vessels, pumps, valves, filters, regulators, sensors, tubing, piping, and specialized installations. Each element needs to work with the chemicals being carried and capable of operating under the needed pressure, temperature, and flow conditions.
The inner surface areas of pipelines and fittings are particularly important due to the fact that they come into straight call with procedure chemicals. Suitable materials can help in reducing deterioration, bit generation, and undesirable chemical communications. Engineers likewise think about connection techniques and system format to decrease areas where deposits might accumulate.

Industrial Applications and Advantages
An Ultra high purity chemical delivery system has applications throughout many technology-driven industries. Semiconductor centers utilize high-purity chemicals during wafer handling, cleansing, etching, and various other construction phases. Drug and biotechnology firms might make use of regulated chemical shipment for study, solution, and making operations.
Other applications consist of solar-cell production, electronic devices producing, labs, and specialized chemical handling. Dependable shipment facilities can help facilities preserve secure process problems while decreasing unnecessary chemical waste. Consistent flow and regulated circulation can likewise add to improved operational performance.
Security and Automated Tracking
Security is an essential factor to consider when taking care of specialized chemicals. Some substances may be harsh, toxic, responsive, or combustible, making proper control and tracking important. An Ultra high purity chemical delivery system can incorporate sensing units and automated controls to keep an eye on important criteria such as pressure, temperature level, circulation price, and leakage.
Automated tracking allows operators to observe system problems better and react to uncommon changes. Appropriate ventilation, secondary control, emergency shutoff systems, and normal examinations can give extra layers of protection. Upkeep programs are similarly essential since worn seals, damaged tubing, or malfunctioning valves can influence both safety and chemical purity. Browse through this website https://www.chengweisemi.com/application/ ready to understand extra.
Future Growths in Chemical Distribution Modern Technology
The future of high-purity chemical distribution is closely gotten in touch with automation, advanced products, digital surveillance, and enhanced procedure control. Intelligent sensing units can provide significantly detailed information regarding system efficiency, while automated control systems can assist keep constant operating problems.
Manufacturers are also checking out methods to minimize waste, improve power effectiveness, and expand tools life. As innovative sectors demand better accuracy, an Ultra high purity chemical delivery system will remain to evolve to meet increasingly strict demands.
Ultimately, successful chemical distribution relies on more than merely moving chemicals from one location to another. It needs cautious system layout, suitable products, contamination control, safety measures, monitoring, and preventive upkeep. Together, these aspects create a reputable foundation for modern accuracy manufacturing.
Reviews